Looking for High Purity Acetone Supplier in India?
Ask any formulation chemist to name a solvent they can't do without, and acetone comes up almost immediately. It's not glamorous. It won't win any awards for being interesting. But it works — fast, clean, predictable — and that's exactly what you want when you're running a production line that can't afford surprises.
We supply Pharma Grade Acetone (CAS 67-64-1) from Ankleshwar, Gujarat — suited for synthesis, extraction, purification, and equipment cleaning in regulated pharmaceutical environments. Its complete miscibility with water and most organic solvents, combined with a low boiling point that leaves no residue behind, makes it one of the more straightforward solvents to work with across different process steps.
Available for both domestic and export supply with full documentation — CoA, MSDS, and technical data on request. If you're currently sourcing Pharma Grade Acetone and want to evaluate us as an alternative or additional supplier, get in touch and we'll respond within one business day.
General Information
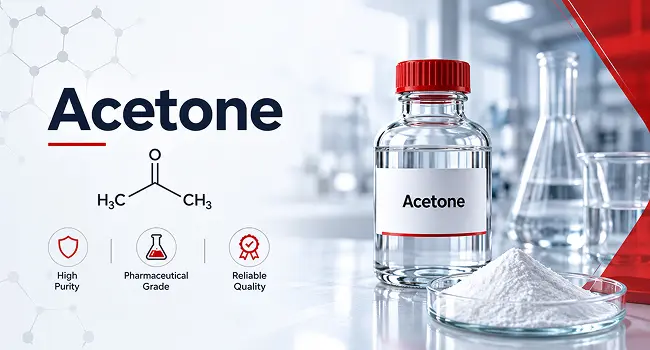
So what is it, exactly? Acetone (CAS Number: 67-64-1) is an invisible yet volatile compound, which can be identified not only by its strong pungent odor but also due to its high solubility to many other compounds – polar and non-polar. Moreover, acetone itself is polar aprotic and it can dissolve just about anything. That's the whole reason it's become such a go-to across industries.
Here's the thing that really makes acetone useful, though: it has a low boiling point and evaporates fast. Once it's done dissolving whatever needs dissolving, it gets out of the way just as quickly. No lingering residue, no drawn-out drying step eating into your timeline. For anyone doing synthesis or purification work, that's not a small perk — it's often the deciding factor in choosing acetone over something else.
In pharma settings, you'll typically see it supplied as Pharma Grade — built to meet the purity bar required for process solvents and excipients in regulated environments. And because it evaporates so cleanly, it's particularly handy anywhere leftover solvent could throw off a finished product or mess with the next step in processing.
One more thing worth mentioning: acetone plays nicely with a huge range of reagents and substrates. Formulation chemists don't need five different solvents for five different jobs — acetone often just... handles it.
Applications
Acetone serves multiple critical functions across organic synthesis, purification, and manufacturing:
Reaction and purification solvent
Shows up constantly in organic synthesis, especially nucleophilic substitution reactions and purification steps, simply because it dissolves so much.
Equipment cleaning and degreasing
The unsung hero of changeovers. Cleans manufacturing equipment between production runs without leaving anything behind.
Extraction processes
Used in extraction and crystallization steps throughout pharmaceutical manufacturing.
Process solvent for intermediates
Quietly essential in producing and purifying pharmaceutical intermediates.
Recrystallization
A common choice when purifying solid compounds during API and intermediate manufacturing.