Looking for High Purity Ethyl Acetate Supplier in India?
If you've ever caught a faint, fruity whiff near a pharma production floor, there's a decent chance ethyl acetate is somewhere nearby. It's one of those solvents that quietly does a lot of heavy lifting — extractions, coatings, purification — without ever really announcing itself. Not the flashiest chemical in the plant, but try running certain processes without it and you'll notice the gap fast.
We supply Pharma Grade Ethyl Acetate (CAS 141-78-6) from our facility in Ankleshwar, Gujarat. It's particularly well suited for extraction steps, tablet coating, and chromatographic separation in pharmaceutical manufacturing — where its low toxicity profile and fast evaporation make it a practical choice over harsher solvents. Supplied to meet pharmacopeial purity requirements, with documentation in place for regulated environments.
Whether you need it for a specific process stage or as a regular production solvent, we can discuss quantities, lead times, and documentation. Domestic and export supply available — contact us and we'll get back to you within one business day.
General Information
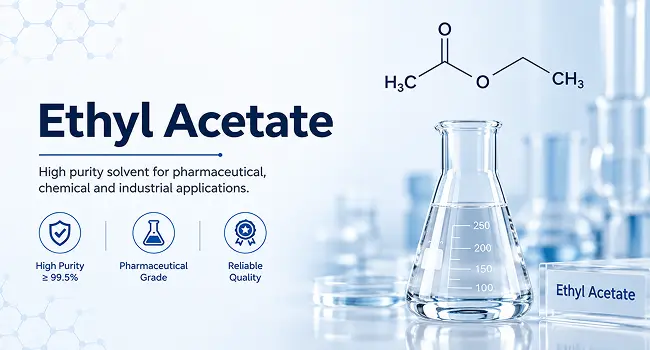
Ethyl Acetate (CAS No. 141-78-6) is an ester obtained from ethanol and acetic acid, and I must admit that ancestry accounts for quite a lot for its nature, because ethyl acetate is a colorless liquid with a pleasant scent and acts as a polar aprotic solvent, meaning "it is a good solvent for a number of substances." It is very soluble in other organic solvents and highly volatile.
What makes it genuinely useful in pharma settings is its low toxicity relative to a lot of alternative solvents, paired with strong solvency for resins, oils, and cellulose derivatives. That combination shows up a lot — chromatography, extractions, formulation work, purification steps. When it's supplied at Pharma Grade, it's built to meet the purity and impurity thresholds that regulated drug manufacturing demands, which is a different bar entirely from the industrial-grade version used in, say, printing inks or adhesives.
There's also something practical about its volatility. Fast evaporation means less residual solvent left behind in a finished product, and in pharma, that's not just a convenience — it's often a regulatory requirement. Nobody wants trace solvent showing up where it shouldn't.
Applications
Ethyl Acetate plays a vital role across key pharmaceutical and manufacturing functions:
Extraction processes
Commonly used to extract active compounds from botanical or biological source material, thanks to its solvency and low toxicity.
Purification and crystallization
Plays a role in purifying intermediates and APIs during downstream processing.
Chromatography
Used as a mobile phase component in TLC and HPLC work, where consistent purity really matters.
Topical formulation processing
Applied in certain topical drug preparation processes, given its compatibility with a range of active ingredients.
Coating and film-forming applications
Used in some pharmaceutical coating processes, where its fast evaporation helps form even, residue-free films.