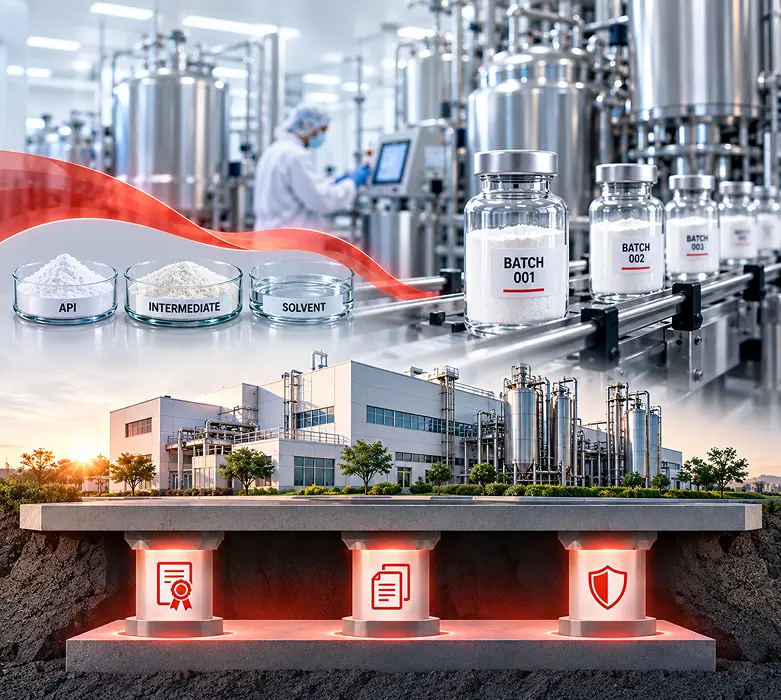
Behind every batch of API, intermediate, or solvent we ship, there's a facility built specifically to keep that batch consistent with the one before it and the one after it. Facilities don't usually get much attention in a sourcing decision, but they're really the foundation everything else — certifications, documentation, reliability — actually rests on.
Manufacturing
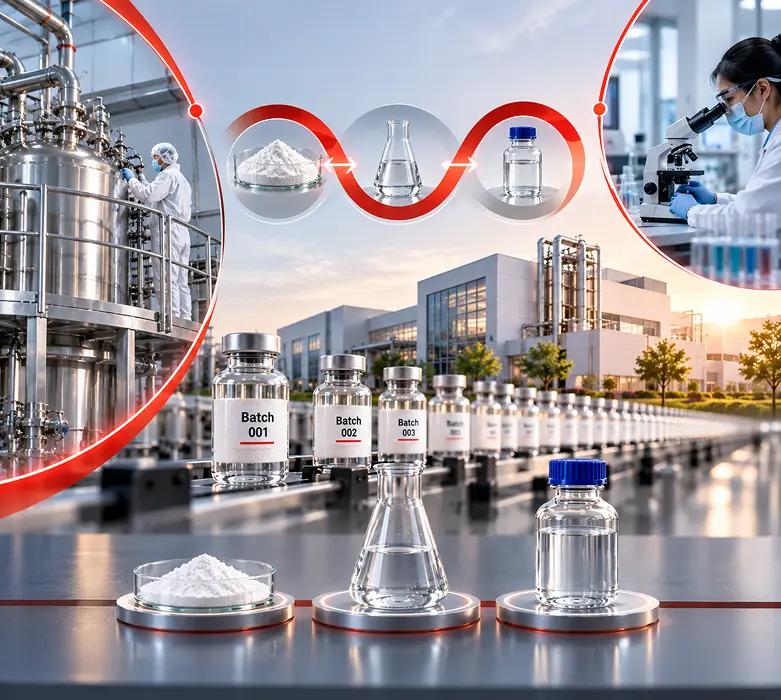
With a successful performance record of over 24 years, we manufacture, export, and supply Active Pharmaceutical Ingredients (APIs) and Intermediates through our site in Ankleshwar, Gujarat. Our facilities are designed to handle multiple products, with dedicated solvent recovery plants built into the production process — a detail that matters both for cost efficiency and environmental responsibility, since recovered solvents reduce waste rather than treating every batch as a one-way input.
Our API and Intermediate facilities are inspected and approved by various global regulatory bodies and meet WHO-GMP compliance standards. That's not a small claim — international regulatory inspection means the facility has been independently verified against globally recognized manufacturing standards, not just self-certified. For manufacturers and formulators sourcing raw materials from us, that inspection history translates directly into confidence that what arrives at their dock matches what's on the specification sheet, batch after batch.
Continuous Improvement
Our highly-skilled team of engineers and chemists focuses on continuous improvement of product quality and yield — meaning the facility isn't static. Processes get refined over time, which is part of how a manufacturer sustains consistent output across 24+ years without quality drifting.
R&D
Manufacturing consistency doesn't happen by accident — it depends on the technical groundwork done well before a product ever reaches commercial scale. Our approach to product development and process refinement sits behind everything from the specifications our APIs meet to the consistency formulators have come to expect batch after batch.
Process Optimization & Yield Refinement
That work spans several fronts. Process optimization is a continuous effort, not a one-time exercise — refining reaction conditions, yield, and purity profiles for existing products like our Lidocaine APIs and Chlorhexidine derivatives, so that what we manufacture today performs at least as consistently as what we manufactured years ago, if not better. This kind of ongoing refinement is part of why a facility with 24+ years of operating history can still claim continuous improvement in product quality and yield — it's not a static production line running the same process unchanged since day one.
Technical Development & Portfolio Addition
Technical development also plays a role in how new pharmaceutical intermediates and solvent grades get evaluated and brought into our product range, ensuring that anything we add meets the same purity, consistency, and documentation standards as our established products before it's offered commercially. That discipline matters particularly for regulated pharmaceutical inputs, where a rushed or under-characterized addition to a product line can create downstream problems for every customer relying on it.
Regulatory & Analytical Documentation
Beyond process work, our technical teams support the documentation side of R&D too — generating and maintaining the analytical data, specifications, and technical files that back our Drug Master Files and regulatory submissions. That connective tissue between lab-level technical work and formal regulatory documentation is often what separates a supplier customers can build a validated formulation around from one they can't.
Documented Performance Guarantee
Ultimately, the goal of this technical groundwork is straightforward: every product leaving our facility should perform exactly as documented, every time, whether it's going into a client's trial batch or a long-running commercial supply agreement.
Quality
Quality control runs through every stage of our operation, backed by a certification portfolio that includes WHO-GMP, FDA, Written Confirmation (WC), ISO 9001:2015, ISO 14001:2015, ISO 45001:2018, and HALAL certification. We maintain Drug Master Files — both Open and Closed Part — across our product range, giving customers the documentation trail they need for their own regulatory submissions.
This isn't just paperwork sitting in a drawer somewhere. These certifications require ongoing compliance, periodic audits, and demonstrated consistency — which is precisely why formulators and manufacturers treat a well-documented supplier as lower-risk than one without this kind of regulatory backing in place.
Quality Certifications
- WHO-GMP Certified
- Local FDA Compliant
- Written Confirmation (WC)
- ISO 9001:2015, 14001:2015, 45001:2018
- HALAL Certified
- Open & Closed Part DMFs
Why Choose Us
24+ years of manufacturing performance
with facilities inspected and approved by global regulatory bodies
Dedicated solvent recovery systems
supporting both cost efficiency and environmental responsibility
WHO-GMP compliant facilities
for both API and Intermediate production
Comprehensive certification portfolio
WHO-GMP, FDA, WC, ISO 9001:2015, ISO 14001:2015, ISO 45001:2018, HALAL
Open and Closed Part DMFs maintained
across our product range, supporting customer regulatory filings